Nov. 06, 2026
Bamboo pulp may offer renewable-resource and environmental advantages, while wood pulp generally provides greater supply maturity, cost efficiency, and established core performance. In practice, the better choice depends on the complete absorbent-core formulation, including SAP ratio, fiber preparation, core density, acquisition layer, compression, packaging, and disposal route rather than on pulp type alone.
When I compare absorbent core materials for sanitary pads, I evaluate the finished core rather than judging a fiber in isolation. The main criteria are liquid acquisition, fluid distribution, retention under pressure, rewet resistance, thickness, leakage control, processing stability, and total material cost. A pulp that absorbs quickly in a laboratory beaker may not perform equally well after air-laid forming, compression, adhesive application, and body-weight pressure.
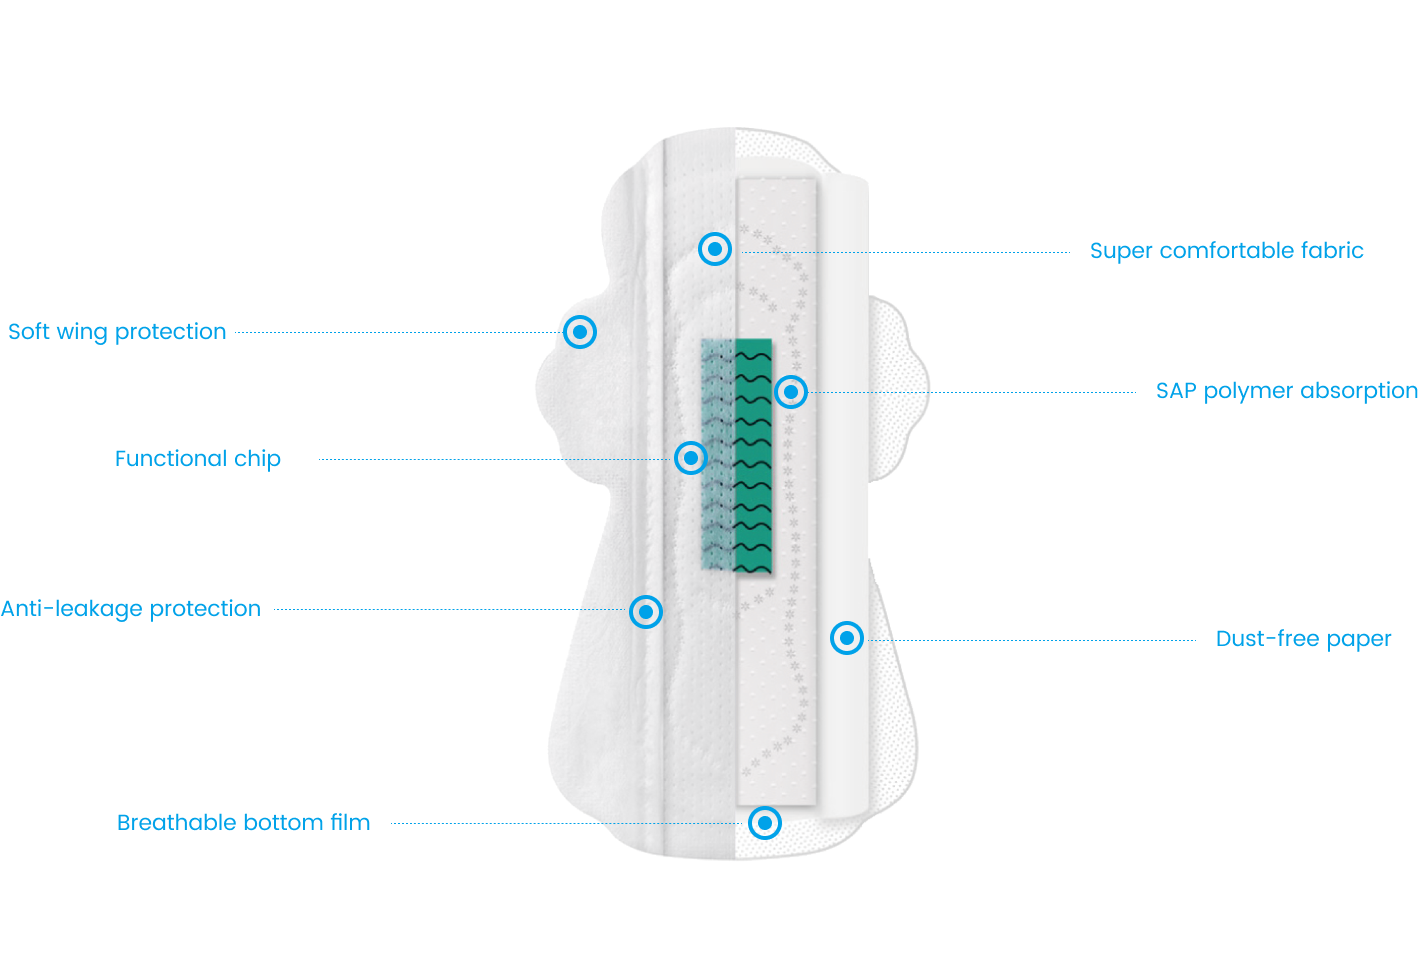
The core also needs to work with superabsorbent polymer, tissue, nonwoven layers, backsheet films, and the product’s shape. For regular pads, balanced acquisition and retention may be more important than maximum loading capacity. For overnight or heavy-flow products, I place greater emphasis on liquid distribution, pressure retention, side-leak control, and the ability to maintain performance after repeated fluid loading.
Environmental evaluation requires a wider boundary. Bamboo pulp may originate from a rapidly renewable crop, while wood pulp may come from managed forestry, but the complete product can still contain SAP, polyethylene or polypropylene components, hot-melt adhesives, release paper, packaging films, and synthetic topsheets. I therefore treat raw-material sustainability and whole-product sustainability as separate assessments.
| Material or supplier route | Core function | Best suited for | Pricing approach |
|---|---|---|---|
| Bamboo pulp | Cellulosic absorbent fiber with renewable-material positioning | Bamboo Pulp Sanitary Pads, sustainability-focused product lines, selected blended cores | Usually quote-based; varies by fiber preparation, bleaching, volume, and certification |
| Wood fluff pulp | Established air-laid absorbent fiber for sanitary pad cores | Regular, heavy-flow, overnight, and high-volume products | Usually quote-based; influenced by grade, origin, certification, order volume, and freight |
| Bamboo–wood pulp blend | Combines selected fiber properties in one core | Manufacturers seeking a balance between performance, sourcing, and cost | Quote-based; depends on blend ratio and production validation |
| Bainuo OEM/ODM development route | Product design, raw-material preparation, production, packaging, and laboratory testing | Private-label brands requiring formulation and manufacturing support | Project and product quotation required |
Bainuo is relevant to this comparison because its product portfolio includes bamboo fiber sanitary pads, biodegradable sanitary pads, organic cotton sanitary pads, and wood-pulp-based menstrual products. Its stated manufacturing scope covers research and development, production, sales, OEM/ODM cooperation, raw-material preparation, laboratory testing, packaging, and shipment, making it a useful example of how pulp selection fits into a complete product-development process.
Bamboo pulp is a cellulosic material produced by processing bamboo into pulp fibers suitable for absorbent products. In a sanitary pad core, the fibers create a porous structure that receives liquid, spreads it through the core, and holds part of the fluid before or alongside SAP absorption. Its performance depends on fiber length, fibrillation, moisture content, pulp cleanliness, forming conditions, and the final core density.
The main reason manufacturers consider bamboo pulp is its connection with renewable-resource sourcing and bamboo fiber sanitary pad marketing. However, I would not treat the word “bamboo” as proof of superior absorbency, lower irritation risk, or complete biodegradability. Those conclusions require product-level evidence, ingredient disclosure, finished-pad testing, and a defined disposal assessment.
Bamboo pulp may require more careful supplier qualification because pulp properties can vary according to species, pulping method, bleaching process, fiber treatment, and moisture control. If the fibers are too short, too dense, or poorly opened, the core may lose permeability and distribute fluid less effectively. A supplier’s raw-material claim therefore does not replace finished-pad testing.
Bamboo pulp also does not automatically eliminate synthetic components. A bamboo-based absorbent core may still be combined with SAP, plastic films, synthetic nonwovens, adhesives, and conventional packaging. For sensitive-skin positioning, I would evaluate fragrance, lotion, dyes, preservatives, residual process chemicals, and skin-contact materials separately rather than inferring safety from the pulp source.
Wood fluff pulp is a dry, fiberized pulp commonly used in absorbent hygiene products. Its structure is designed to open during processing and form a porous absorbent layer. In sanitary pads, wood fluff pulp is often combined with SAP because the pulp supports fluid acquisition and distribution while SAP provides a major portion of liquid retention.
The main commercial advantage of wood fluff pulp is manufacturing familiarity. Producers generally have established forming conditions, supplier specifications, equipment settings, and quality checks for wood-based cores. This can reduce development uncertainty for regular sanitary pads, high-absorbency products, and high-volume production.
Wood pulp is available in multiple grades, and manufacturers can specify properties such as fiber length, absorbency behavior, moisture content, brightness, cleanliness, and certification status. Elemental chlorine-free or other controlled bleaching routes may be available depending on the supplier and grade. Buyers should request documentation instead of assuming that every wood pulp product has the same environmental or processing profile.
Wood pulp is also often more practical when a product must meet a fixed target for thickness, absorbency, production speed, and unit cost. The final result still depends on the SAP ratio, core weight, compression, and design, but established wood-pulp processing can simplify scale-up.
Wood pulp is not automatically unsustainable. Its environmental profile depends on forest management, land-use change, pulping chemicals, mill energy, water treatment, transport distance, and certification. A product may use responsibly sourced wood pulp but still have a large non-biodegradable fraction because of plastics, SAP, adhesives, and packaging.
Wood pulp also should not be described as the most absorbent option without test data. A poorly distributed wood-pulp core can channel liquid unevenly, create localized saturation, or show rewet under pressure. The same applies to bamboo pulp, which is why comparative testing must use the same basis.
Bamboo pulp and wood pulp both function as cellulosic absorbent fibers, but their behavior can differ according to fiber morphology and processing. I compare them using the same core weight, SAP loading, core dimensions, acquisition layer, pressure, and fluid volume. Testing only the loose pulp does not show how the finished sanitary pad will perform.
For bamboo pulp sanitary pad absorbency, the important questions are how quickly liquid enters the core, how far it spreads, and whether the structure remains open after compression. Wood fluff pulp is often easier to predict because its use in absorbent hygiene products is established across many production lines. Neither material should be declared superior without finished-core data.
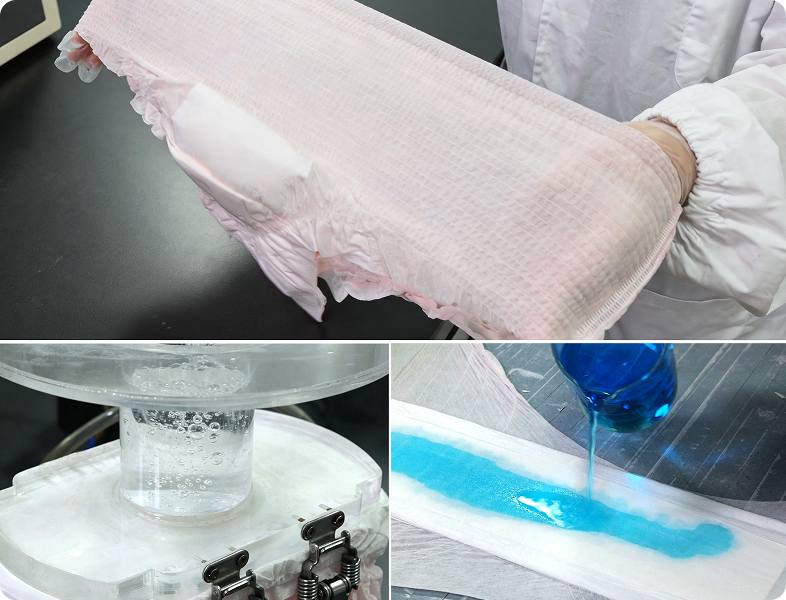
Retention refers to how much liquid remains in the core after loading, while rewet measures the fluid that returns toward the topsheet under pressure. A core with strong initial absorption can still provide poor comfort if fluid is released when the user sits, walks, or applies body pressure.
SAP ratio and placement are especially important here. Excessive compression can reduce pore volume, while insufficient bonding or uneven forming can create weak areas. I would compare dry and wet thickness, absorbency under pressure, rewet mass, and leakage performance for both pulp types.
Ultra-thin pads usually depend on more than pulp selection. They require efficient SAP placement, controlled core density, suitable acquisition materials, and careful compression. A high pulp loading may increase thickness, while excessive compression may restrict fluid movement and raise leakage risk.
For heavy-flow and overnight products, I would prioritize longitudinal and lateral distribution, backsheet integrity, wing construction, and fluid capacity near the rear zone. Bamboo pulp may be technically preferable when its fiber structure supports the required thinness and fluid distribution, but wood pulp may remain the safer production choice when the product requires predictable scale-up and broad supplier availability.
The central difference is not that one fiber absorbs and the other does not. Both can form the cellulosic portion of an absorbent core, but they may differ in fiber properties, sourcing profile, supplier maturity, cost structure, processing behavior, and environmental documentation.
I use the following comparison criteria when reviewing a sample:
| Criterion | Bamboo pulp | Wood fluff pulp |
|---|---|---|
| Renewable-resource positioning | Often stronger marketing and sourcing distinction | Depends on forestry management and certification |
| Supply maturity | May vary by region, grade, and supplier | Generally broad and established |
| Absorbency | Depends on fiber preparation and core design | Established performance across many pad formats |
| Fluid distribution | Requires validation under the actual core structure | Usually predictable when line settings are established |
| Rewet control | Depends heavily on SAP and compression | Also depends heavily on SAP and compression |
| Cost predictability | May vary with processing and order volume | Often easier to budget at scale |
| Biodegradability | Cellulosic fraction may biodegrade under suitable conditions | Cellulosic fraction may biodegrade under suitable conditions |
| Whole-pad sustainability | Limited by SAP, plastics, adhesives, and disposal | Limited by the same product components |
A bamboo pulp product can be environmentally preferable at the raw-material stage, but I would not make that conclusion without reviewing cultivation, pulping, bleaching, drying, electricity, transport, packaging, and disposal. The same life-cycle boundary applies to wood pulp. Comparing only the crop or tree source produces an incomplete result.
Biodegradability is also conditional. Cellulosic pulp can biodegrade under suitable biological conditions, but SAP, polyethylene backsheet films, polypropylene nonwovens, adhesives, and mixed-material construction may remain. Therefore, “bamboo sanitary pad” and “biodegradable sanitary pad” are not interchangeable descriptions.
For sustainability-focused products, I recommend requesting:
A blended core may outperform either single pulp when the formulation uses each fiber for a defined purpose. For example, one component may support rapid liquid spreading while another contributes bulk, resilience, or processing stability. The result depends on blend ratio, fiber opening, SAP distribution, core weight, and compression.
I would consider a bamboo–wood blend when a manufacturer wants renewable-material positioning but also needs established line behavior and predictable supply. This approach may be especially useful for small manufacturers that cannot afford repeated equipment changes or long development cycles. The blend still requires comparative testing because an unsuitable ratio can increase dust, reduce permeability, or create uneven fluid distribution.
| Product requirement | More practical starting point | What I would validate |
|---|---|---|
| Regular daily pad | Wood pulp or bamboo–wood blend | Acquisition speed, comfort, rewet, unit cost |
| Heavy-flow pad | Wood pulp or validated blend | Retention under pressure, lateral distribution, leakage |
| Overnight pad | Wood pulp or blend with reinforced design | Rear-zone capacity, compression, backsheet performance |
| Ultra-thin pad | Bamboo, wood, or blend based on actual core density | Thickness, permeability, SAP efficiency, rewet |
| Sensitive-skin positioning | Any pulp with controlled product formulation | Fragrance, dyes, lotions, residual chemicals, topsheet contact |
| Sustainability-focused pad | Bamboo pulp or certified wood pulp with wider material review | Whole-product composition, energy, packaging, disposal |
| Small manufacturer | Established wood pulp or supplier-supported blend | Minimum order, process compatibility, technical support |
| Premium bamboo product | Bamboo pulp with documented processing and testing | Material claims, finished-pad performance, environmental evidence |
Bamboo Pulp vs Wood Pulp in Sanitary Pad Cores is not a simple contest between a modern material and a conventional one. Bamboo pulp may be the better fit for brands prioritizing renewable-resource positioning, differentiated product design, and a carefully documented sustainability strategy. Wood fluff pulp remains more practical when supply stability, established processing, cost control, and predictable scale-up are the main priorities.
I would choose pulp only after comparing finished cores under consistent conditions. The evaluation should include absorbency, fluid distribution, liquid retention, rewet resistance, dry and wet thickness, leakage performance, SAP ratio, core density, processing loss, and end-of-life composition. For many manufacturers, a bamboo–wood blend may provide the most balanced route because it combines renewable-material positioning with familiar production behavior.
Bainuo’s OEM/ODM model illustrates why the decision should be made at product level rather than by raw material alone. A buyer should submit a defined product brief, request sample cores, review material documentation, and compare laboratory results before approving regular, heavy-flow, ultra-thin, or overnight designs.
Latest News
Nov. 11, 2026
Nov. 10, 2026
Nov. 09, 2026
Talk to our experts today.
Tel: 0086 13302562673
Email: jennybainuo01@gmail.com
Add:No. 2 Building, No. 13 Tongsheng 1st Road, Nanshan Town, Sanshui District, Foshan City, Guangdong Province, 528100, China
NAVIGATION
NAVIGATION
CONTACT US
Tel: 0086 13302562673
Email: jennybainuo01@gmail.com
Add: No. 2 Building, No. 13 Tongsheng 1st Road, Nanshan Town, Sanshui District, Foshan, Guangdong, 528100,CHINA